Four-quadrant
operation
Motoring and regenerative operation in both directions, engineered around the application’s load cycle.

DC-to-AC Drive Modernization · Multi-Motor Roller Conveyors · Low-Harmonic Regenerative Technology
INOMAX supplied an engineered ACS880 regenerative drive system for the steel plant’s AC motor application, combining multi-motor control, AFE-based cabinet engineering and competitive project pricing.
01 / PROJECT OVERVIEW
DC-to-AC drive modernization with four-quadrant regenerative technology for an Indonesian steel plant.
The customer previously used a legacy DC motor and drive arrangement. Its modernization project moved to an AC motor drive solution, with machinery and motors sourced from an Italian supplier and the drive system supplied by INOMAX. This case focuses on the multi-motor roller conveyor drive package.
INOMAX configured a four-quadrant, low-harmonic regenerative AC drive solution around the approved motor groups and electrical design. The package combines Active Front End (AFE) supply, a common DC bus, motor-side inverter modules and engineered drive cabinets.
The project partner, a system integrator supplying ABB and Siemens solutions, evaluated both ABB and INOMAX proposals. Lower project pricing and a shorter lead time supported the INOMAX offer; factory and steel-plant reference visits gave the customer confidence to proceed.
02 / PROJECT REQUIREMENTS
The modernization combined the transition to AC motors with motor-group selection, regenerative power-flow requirements and practical cabinet engineering.
The end customer needed equipment urgently and was sensitive to price. Technical suitability, delivery lead time and purchase cost all influenced the final supplier decision.
03 / INOMAX SOLUTION
The project package combined four-quadrant regenerative capability with a multi-cabinet arrangement tailored to the roller conveyor system.
Motoring and regenerative operation in both directions, engineered around the application’s load cycle.
Active Front End architecture integrated with the project’s filter and electrical design.
Drive ratings and motor grouping based on the approved motor schedule.
TR5 and TR6 cabinet layouts for an integrated industrial drive lineup.
During suitable deceleration, braking or other generating conditions, a regenerative drive system can return eligible motor braking energy to the electrical supply. This provides an alternative to dissipating that energy as heat in braking resistors.
Where steel rolling or roller conveyor duties involve braking and reversing, energy recovery can reduce net energy drawn from the grid. The result depends on the load profile, braking frequency, operating cycle and system configuration.
The low-harmonic drive architecture combines active power conversion with the project’s filter and electrical design. Harmonic performance and regenerative operation must be evaluated for the actual network and operating conditions.
A common DC bus serves multiple SMM inverter modules. Each module is selected for its assigned roller motor group or individual auxiliary duty, keeping the configuration tied to the approved motor schedule.
ILLUSTRATIVE POWER FLOW
↓Output reactor↓
Roller motor group
↓Output reactor↓
Roller motor group
↓Output reactor↓
Roller motor group
Public-facing architecture illustration, not an installation or wiring drawing. Individual motor protection is a separate part of the project integration scope.
Motoring: power flows from the electrical supply through the AFE and common DC bus to the inverter modules and motor groups.
ONE MODULE, MULTIPLE MOTORS
Three examples from the final selection schedule. Select a group to see its motor load and INOMAX module.
6 × 38 A motor nameplate current. Selection is specific to this project’s load and operating requirements.
PROJECT-SPECIFIC ENGINEERING
04 / PROJECT DATA
The final INOMAX motor and drive schedule defines the roller conveyor scope below. These figures describe this drive package, rather than the steel mill’s entire electrical installation.
| Industry | Steel manufacturing |
|---|---|
| Application | Roller conveyor drive system |
| End-user location | Indonesia |
| Project integrator | System integrator supplying ABB and Siemens solutions |
| Drive architecture | Four-quadrant regenerative, low-harmonic AFE system with a common DC bus and modular motor-drive sections |
| Equipment and motors | Sourced from an Italian supplier |
| Drive system supplier | INOMAX |
FINAL MOTOR SCHEDULE
| Drive group | Motors | Motor rated power |
|---|---|---|
| TR5 | 131 | 2,533 kW |
| TR6 | 167 | 1,837 kW |
| Total | 298 | 4,370 kW |
4,370 kW is the sum of connected motor nameplate ratings. It is not the AFE rating or measured simultaneous demand.
Source: final INOMAX roller conveyor motor and drive list, 9 July 2024. Final scope is kept separate from the earlier ABB–INOMAX comparison-stage schedule.
05 / DRIVE SELECTION & CUSTOMER DECISION
The customer compared motor-group configurations, AFE supply, inverter selections and output reactors against the project requirements. The tables below summarize the original proposal-stage selections.
The comparison-stage schedule lists the following arrangement for each of its two supply groups.
Swipe the table to compare both proposals →
| Supply arrangement | ABB proposal | INOMAX proposal |
|---|---|---|
| For each of the two supply groups |
5 units in parallelACS880-907-0900A-3 | 4 units in parallelACS880-2R86-1480A-3 |
AFE comparison from the proposal-stage schedule dated 25 May 2024, repeated for both supply groups. These configurations are shown as proposed; final equipment sizing followed the subsequent project engineering and motor schedule.
Each comparison below pairs the ABB and INOMAX module specified for the listed load, together with the output reactor in the schedule.
Swipe the table to compare both proposals →
| Motor group / connected load | ABB proposal | INOMAX proposal | Listed output reactor |
|---|---|---|---|
| 6 × 18.5 kW111 kW · 228 A | ACS880-107-300A-3 | ACS880-R72-293A-3+SMM | OCL-2.2V/330A |
| 4 × 18.5 kW74 kW · 152 A | ACS880-107-210A-3 | ACS880-R55-206A-3+SMM | OCL-2.2V/230A |
| 5 × 18.5 kW92.5 kW · 190 A | ACS880-107-250A-3 | ACS880-R63-246A-3+SMM | OCL-2.2V/250A |
| 10 × 11 kW110 kW · 230 A | ACS880-107-300A-3 | ACS880-R72-293A-3+SMM | OCL-2.2V/330A |
Source: project ABB–INOMAX comparison schedule, 25 May 2024. These are comparison-stage selections, not the final motor totals. Load values are summed motor nameplate ratings. Model pairings do not establish identical specifications or drop-in interchangeability; the application conditions require engineering review.
The customer evaluated both the proposed drive configurations and commercial terms. INOMAX offered a substantially lower equipment price for the project while addressing the specified drive requirements. The decision also considered lead time, factory capability and operating references. Project pricing is assessed against the agreed configuration and supply scope.
CUSTOMER EVALUATION
INOMAX’s lower price and shorter lead time addressed the immediate project pressures. The customer travelled to China before committing, to see whether the capabilities and operating references supported the offer.
The ABB proposal was substantially more expensive. INOMAX’s lower offer directly addressed the end customer’s sensitivity to equipment cost.
Why it mattered
A better fit for the project’s purchasing budget.
The project was urgent. INOMAX could offer a shorter lead time than the ABB option under consideration, making delivery a key part of the decision.
Why it mattered
An offer better aligned with the customer’s schedule.
The customer assessed INOMAX’s factory and visited existing steel-plant installations in China before selecting the solution.
Why it mattered
Direct evidence of capability and equipment in operation.
BEFORE THE FINAL DECISION
The visit allowed the customer to examine how INOMAX develops and manufactures its drives, and to see the equipment working in a demanding industrial application.
At the INOMAX factory in China, the customer reviewed the company’s R&D strength, production processes and quality-assurance arrangements. The visit also covered INOMAX’s experience supplying alternatives to ABB and Siemens drives in other projects.
INOMAX took the customer to existing steel-plant projects in China, including an installation at Shougang in Beijing. There, the customer saw INOMAX drives operating well in a real steel production environment.
With the factory capability and steel-plant operation assessed in person, the customer weighed technical suitability, price, lead time and the supplier’s project experience, then selected the INOMAX solution.
Competitive pricing and faster availability made INOMAX worth considering. Factory assessment and operating references gave the customer the confidence to choose it.
06 / MANUFACTURING & SITE FEEDBACK
INOMAX manufactured the drive cabinets to the project electrical design, prepared the equipment for shipment and received installation photographs and positive feedback from the customer.
Power modules, internal connections, busbars and local operator interfaces assembled into the engineered lineup.
Protective wrapping and export packaging prepared for the completed industrial drive cabinets.
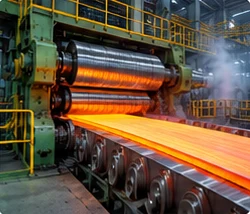
Customer-supplied photographs document the cabinet system and steel rolling application in Indonesia.
Project photographs. Identifying customer markings in the site images have been masked. Select a photograph to enlarge it.
CUSTOMER-REPORTED OUTCOME
The customer shared photographs after delivery and expressed satisfaction with the project. Together with the engineering and manufacturing records, these materials document INOMAX’s supplied drive package. The regenerative system provides energy-recovery capability; actual site energy savings depend on the operating duty and system configuration.
07 / FREQUENTLY ASKED QUESTIONS
Ten answers on energy recovery, DC-to-AC modernization, AFE technology, project scope and multi-motor drive engineering.
A four-quadrant regenerative VFD can return eligible braking energy to the electrical supply during regenerative operating conditions. The actual energy savings depend on the motor load profile, braking frequency, operating cycle and system configuration.
INOMAX can evaluate DC-to-AC drive modernization projects based on motor specifications, mechanical requirements, speed and torque characteristics, control interfaces and the intended operating cycle. The replacement solution must be engineered for the specific application.
INOMAX provides project-specific industrial drive solutions for applications requiring regenerative operation and specialized motor control. In this Indonesian steel mill project, the customer evaluated both INOMAX and ABB proposals and selected INOMAX. Lower project pricing and shorter lead time were part of the decision, alongside factory assessment and operating references. Commercial comparisons depend on comparable equipment configurations, supply scopes and terms.
An Active Front End (AFE) is an active power-conversion stage used between the AC supply and a drive system’s DC link. Depending on the system design, an AFE can provide controlled power conversion and support regenerative power flow back to the electrical supply. AFE selection depends on the application’s power-flow requirements, electrical network, harmonic requirements and overall system configuration. The INOMAX project documentation includes an AFE-based configuration for the steel mill roller conveyor drive system.
Yes. During the project evaluation, the customer considered both ABB and INOMAX drive proposals and selected the INOMAX solution for the project scope. The evaluation involved motor-group configuration, drive selection, power conversion equipment, output reactors and overall electrical system arrangement. This page summarizes the approved technical selections; detailed commercial terms and confidential source documents are not disclosed.
No. The motors and associated equipment were sourced from an Italian supplier, while INOMAX supplied the drive system. INOMAX’s scope included drive configuration, project-specific electrical engineering, cabinet arrangement, manufacturing and delivery of the supplied drive equipment. Responsibilities for installation, commissioning and other site activities are governed by the project contract.
INOMAX can evaluate project-specific drive requirements for steel mills, roller conveyors and other industrial motor control applications. The engineering process may include motor schedule review, drive sizing, multi-motor grouping, electrical topology, cabinet layout, output reactor selection and control interface definition. The final configuration depends on the motor data, operating requirements and agreed project scope.
For a multi-motor drive system, the engineering team typically needs:
These details help determine the appropriate drive rating, motor grouping, protection arrangement and cabinet configuration.
Depending on the agreed project scope, engineering documentation may include motor and drive schedules, electrical single-line diagrams, cabinet layout drawings, drive configuration lists, control I/O lists, connection diagrams and product technical documentation. For this steel mill project, the available materials include motor schedules, TR5 and TR6 cabinet layouts, electrical topology drawings and control interface information.
This project provides a documented example of INOMAX manufacturing and delivering a multi-cabinet drive system for a steel mill roller conveyor application. Project records include cabinet layout drawings, photographs of manufactured equipment, internal cabinet components, export packaging and customer-shared site photographs. Industrial OEMs, system integrators and engineering contractors can contact INOMAX to discuss similar multi-motor VFD systems, high-power drive configurations and customized industrial drive requirements.
DISCUSS YOUR APPLICATION
Send INOMAX your motor specifications, operating cycle and existing drive arrangement to discuss a project-specific regenerative AC drive solution.